LED Strip AQL Inspection Checklist Before You Accept Shipment
- 2026-09-19 13:17
- /
- Arraystar
A pre-shipment inspection based on AQL (Acceptable Quality Limit) sampling catches defects before they leave the factory. Define critical/major/minor defects for LED strip (function, colour, dimensions, waterproofing, packaging), agree the AQL levels and sample size with your supplier, inspect a random sample from finished packed goods, and require test data and corrective action. A written checklist applied consistently turns vague ‘good quality’ claims into enforceable acceptance criteria.
What AQL Inspection Means
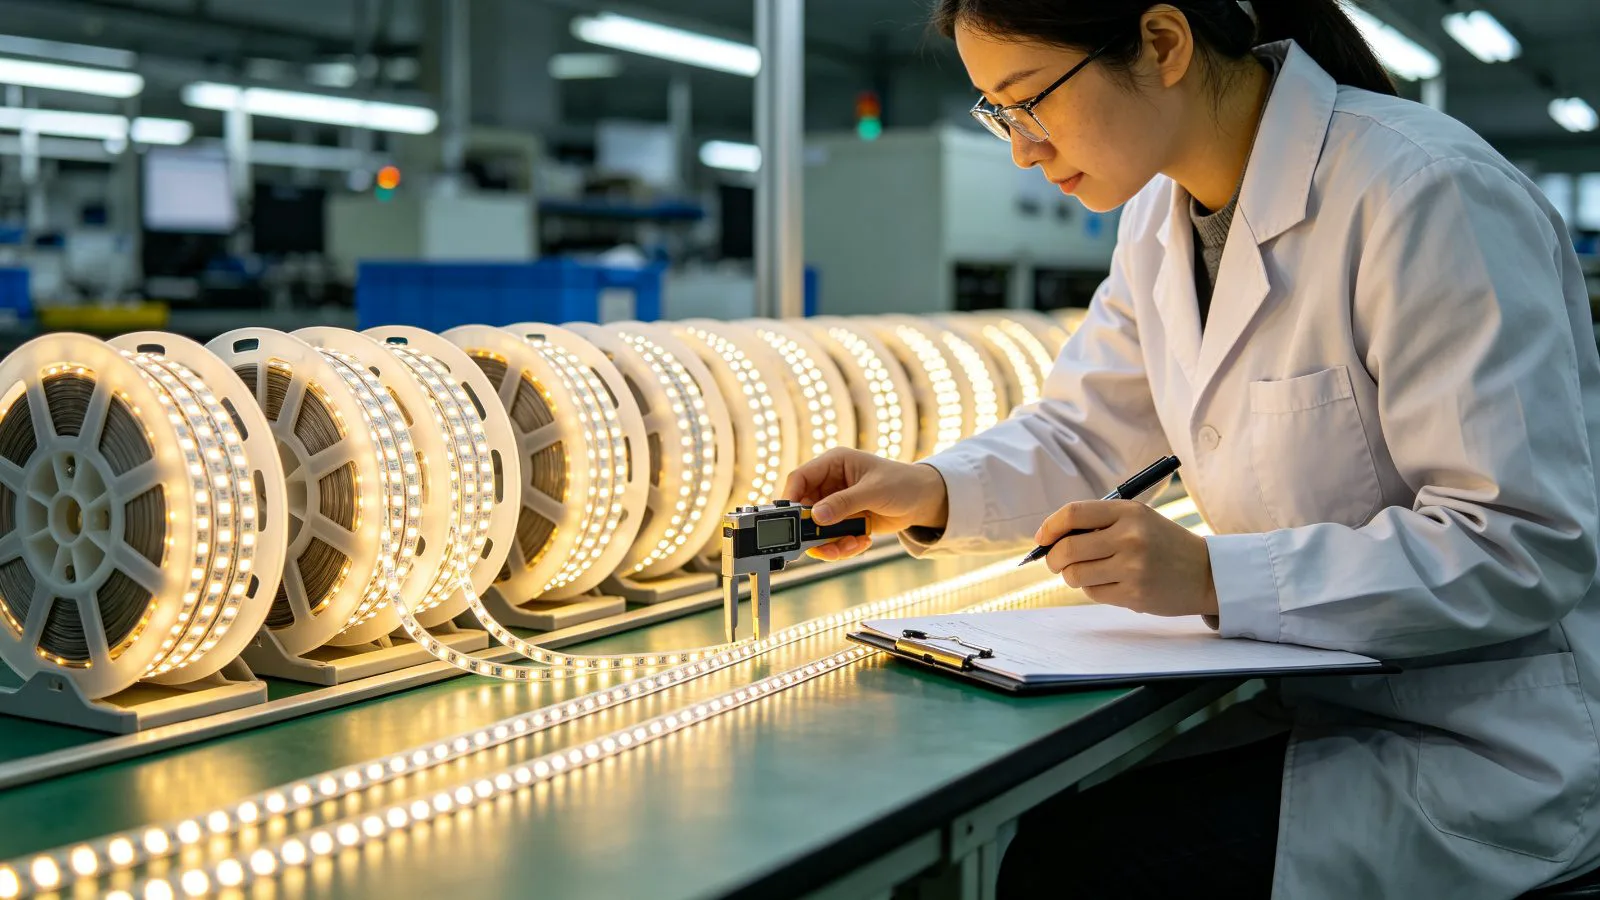
AQL (Acceptable Quality Limit) is a statistically based sampling method widely used in product inspection (associated with standards such as ISO 2859-1 / ANSI Z1.4, derived from military sampling tables). Instead of checking every unit, the inspector draws a defined random sample size from a production lot based on the lot size and chosen inspection level, then accepts or rejects the lot according to how many defects are found and the agreed AQL. Defects are classified by severity: critical (safety/hazardous, e.g. unsafe electrical), major (functional or obvious appearance failures) and minor (small deviations from specification). For LED strip, a pre-shipment inspection (PSI) on finished, packed reels is the buyer's last practical gate before goods ship.
- Random sample from the actual finished lot — not samples hand-picked by the factory.
- Severity classes: critical (safety), major (function/appearance), minor (cosmetic/packaging).
- Sample size from standard tables based on lot quantity and inspection level.
- Accept/reject numbers set by the agreed AQL for each severity.
- Document and photograph defects; reject or rework lots that exceed limits.
LED Strip Defect Classification
Example defect categories (agree exact limits with supplier)
| Class | LED strip examples |
|---|---|
| Critical | Insulation/electrical safety failure, shock risk, non-compliant materials, fire hazard |
| Major | Dead sections/LEDs, wrong colour/CCT, severe bin variance, flicker, wrong voltage, failed waterproofing, wrong length/width |
| Major | Drivers/controller DOA, connectors fail, solder joints open, delaminating adhesive |
| Minor | Slight mark on reel, label/printing error, non-critical packaging dent, minor cosmetic spot |
| Minor | Loose accessories, documentation omission, reel winding untidiness |
Typical commercial AQL settings might use zero tolerance for critical defects and progressively more permissive limits for major and minor (commonly cited values such as 0 / 2.5 / 4.0), but the right levels are a commercial agreement — safety-critical or branded projects warrant stricter limits. Put the agreed AQL, defect definitions and who pays for re-inspection in the purchase contract/QC agreement.
On-Site Inspection and Test Checklist
- Quantity and packing: reel count, metreage, carton counts against the order; packaging intact and correctly labelled.
- Power-on test: light every sampled reel (and controllers/drivers); check for dead LEDs, dead sections, flicker and smooth dimming.
- Colour and bin: compare CCT/colour against the agreed bin and a reference; check uniformity along and between reels.
- Dimensional checks: width, PCB thickness, cut marks, reel length, connector and profile fit.
- Waterproof product: verify IP construction, sealed ends, jacket integrity and (where specified) sample water-pressure/aging evidence.
- Workmanship: solder joints, component placement, adhesive backing, silicone extrusion consistency, no contamination.
- Labelling & docs: correct model, voltage, CCT, batch labels; CE/RoHS marks; test reports and packing list.
Functional/aging tests to request
| Test | What it catches |
|---|---|
| Full power-on / aging | Infant-mortality failures, dead LEDs |
| Dimming sweep | Flicker, dead travel, colour shift |
| Colour/bin comparison | Mixed bins, wrong CCT |
| Voltage test | Wrong-voltage product, driver faults |
| Adhesion pull/peek | Backing/double-sided tape failure |
| Waterproof inspection | Sealing and IP defects |
Process, Sampling and Protecting Yourself
- Inspect after production and packing, before shipment (PSI), ideally with an agreed earlier during-production (DUPRO) check for large/complex orders.
- Sample randomly across cartons and batches; ensure the inspector selects cartons, not the factory.
- Require factory aging/test records and bin data for the lot, not just the golden sample.
- Define accept/reject, rework and re-inspection terms and payment milestones in the contract.
- For first production of a custom product, consider 100% functional test or a tighter inspection level.
- Keep a approved golden sample and signed spec sheet as the comparison standard.
Information to agree before production
| Item | Detail |
|---|---|
| AQL levels | Critical/major/minor limits |
| Defect list | Written, with photos/examples |
| Spec / golden sample | Signed reference standard |
| Inspection timing | DUPRO and/or pre-shipment |
| Re-inspection cost | Who pays after a fail |
| Test data | Aging, bin, waterproof records |
We build pre-shipment QC into production: full power-on aging, bin consistency, dimensional and waterproof checks, and packed-goods inspection against an agreed checklist, and we support customer or third-party AQL inspections with random carton access and lot test records. Send us your AQL levels and defect list and we will align QC acceptance criteria before the order is placed.
Recommended Products
Frequently Asked Questions
What AQL levels should I use for LED strip?
A common commercial starting point is zero critical defects, AQL 2.5 for major and 4.0 for minor, but the correct levels are a commercial agreement based on product value, brand risk and safety exposure; safety-critical, medical or premium projects use stricter limits. Define defect classes and limits in the QC agreement before production.
When should a pre-shipment inspection happen?
After production is complete and goods are packed (typically when at least ~80–100% is finished and export-packed), before shipment, with the inspector drawing a random sample across cartons. For large or custom orders add a during-production (DUPRO) inspection to catch issues early when rework is cheaper.
How is the AQL sample size determined?
From sampling tables (such as ISO 2859-1/ANSI Z1.4) using the lot size and an inspection level (General Level II is common), which yields a code letter, sample size and accept/reject numbers for each AQL. The inspector then randomly draws that number of units from the finished lot.
What are the most common major defects in LED strip?
Dead LEDs or dead sections, wrong CCT or mixed colour bins, visible colour variance along a run, flicker or poor dimming, wrong voltage or length, failed waterproof sealing on IP-rated product, open solder joints and delaminating adhesive. Electrical safety failures and non-compliant materials are treated as critical.
Should I inspect waterproof LED strip differently?
Yes: in addition to function and appearance, verify sealed cut ends and connectors, jacket/extrusion integrity, correct IP rating construction and the factory's water-pressure/aging or test records; where feasible include sample ingress testing in the inspection plan because a sealing defect is a major failure that only appears after installation outdoors.
Placing an order and want pre-shipment QC?
We run power-on aging, bin consistency, dimensional and waterproof checks and support customer/third-party AQL inspection with random carton access and lot records. Send your AQL levels and defect list and we will align acceptance criteria before production.
Email: info@arraystarled.com | Phone: +86-0755-2103-6746 | WhatsApp: 0086 1581 8514 077
Need to size your power supply? Use our LED Strip Power Calculator to find the right driver in seconds.